Compressed air powers tools, actuators, packaging lines, and process controls across factories. Yet a small pressure error can affect machine performance, increase air consumption, or trigger an avoidable shutdown. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook notes that compressed air can represent about 10% of electricity use in manufacturing, and substantially more in some facilities. A gauge cannot eliminate system waste, but it helps operators spot pressure changes where they matter.
Choosing a Pneumatic Pressure Gauge is not just a matter of matching a dial to a pipe. Buyers should compare pressure range, accuracy, connection type, case material, readability, vibration resistance, and suitability for the working environment. ASME B40.100 provides recognized guidance for pressure-gauge design, construction, and testing. Still, compliance alone does not guarantee the right fit for every installation. A gauge beside a vibrating compressor may need different protection than one mounted on a clean, steady panel.
This Top 10 guide gives industrial buyers a practical shortlist for comparing common gauge options. It focuses on useful specifications and real operating conditions, rather than headline features alone. Check the expected pressure against the gauge’s scale, and consider how often readings must be checked or recorded. Small details count. A readable face, secure fitting, and suitable pressure range can make routine inspections clearer. Product claims should still be verified against current manufacturer datasheets; selection depends on the application, and no single model suits every plant.
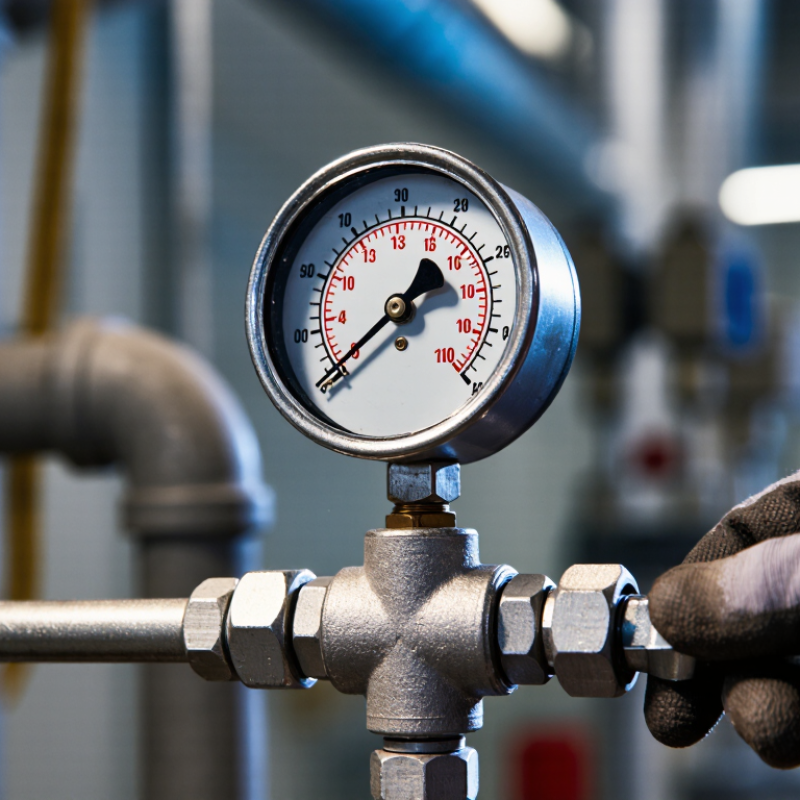
A pneumatic pressure gauge converts compressed air pressure into movement on a dial. Inside a common Bourdon-tube gauge, pressure makes a curved metal tube flex. A linkage transfers that motion to the pointer. The dial then shows pressure, often in psi or bar. A gauge measures pressure at its connection point, not airflow through the line. A small but important distinction.
The U.S. Department of Energy’s Improving Compressed Air System Performance guide says compressed air uses about 10% of industrial electricity, with higher shares at some facilities. The guide also notes that leaks can waste 20–30% of compressor output in poorly maintained systems. A pressure gauge helps operators spot falling pressure, but it cannot locate a leak by itself. Readings are most useful when compared at consistent points and operating conditions.
For industrial selection, check the pressure range, connection size, accuracy class, and resistance to vibration. A gauge running near the end of its scale may be harder to read and less suitable for routine monitoring. Mount it where operators can see it, away from excessive heat and impact. Calibration matters, too. A dial can look convincing while drifting out of tolerance. That is easy to overlook.
A pneumatic gauge should be selected by its working range, accuracy, connection, and environment—not dial size alone. ASME B40.100 identifies Grade 2A accuracy as ±0.5% of span, a useful benchmark when comparing readings. A 0–10 bar gauge with that grade can deviate by about 0.05 bar across its scale. Yet expected operating pressure matters: a needle sitting near the bottom of the dial is harder to read precisely. Choose a range that keeps normal pressure comfortably within the scale, and check whether the specification states accuracy as a percentage of span or reading. Those are not interchangeable.
Look closely at the process connection and wetted materials. Match thread type, port position, and material compatibility to the installation; a mismatch can create leaks or corrosion. For vibrating compressor lines, compare case construction, damping, and liquid filling, while checking temperature limits and overpressure ratings. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook estimates that leaks can waste 20–30% of compressor output. A gauge cannot diagnose leakage alone, but stable, repeatable readings can help operators spot pressure changes worth investigating. Not proof, though. Also compare dial visibility, calibration documentation, and serviceability. A neat specification sheet still cannot predict every vibration spike, so field conditions deserve a trial.
| No. | Gauge Configuration | Measuring Range | Accuracy Class | Dial Size | Process Connection | Wetted Parts | Case / Window | Typical Application |
|---|---|---|---|---|---|---|---|---|
| 1 | General-purpose Bourdon tube gauge | 0–10 bar (0–145 psi) | 1.6 | 63 mm | G 1/4 bottom entry | Copper alloy | Painted steel case / safety glass | Routine pressure indication on compressed-air lines and regulators |
| 2 | High-visibility Bourdon tube gauge | 0–10 bar (0–145 psi) | 1.0 | 100 mm | G 1/2 bottom entry | Copper alloy | Stainless-steel case / safety glass | Panel or equipment readings where improved readability is useful |
| 3 | Low-pressure diaphragm gauge | 0–1 bar (0–14.5 psi) | 2.5 | 100 mm | G 1/2 bottom entry | Stainless-steel diaphragm and connection | Stainless-steel case / safety glass | Low-pressure air circuits and sensitive pneumatic processes |
| 4 | Medium-range Bourdon tube gauge | 0–16 bar (0–232 psi) | 1.6 | 63 mm | 1/4 NPT bottom entry | Copper alloy | Stainless-steel case / polycarbonate window | Compressed-air equipment operating above common 10-bar line pressure |
| 5 | High-range Bourdon tube gauge | 0–25 bar (0–363 psi) | 1.6 | 100 mm | G 1/2 bottom entry | Stainless steel | Stainless-steel case / safety glass | Higher-pressure pneumatic machinery and test systems within the selected range |
| 6 | Vacuum gauge | −1–0 bar (−14.5–0 psi) | 2.5 | 63 mm | G 1/4 bottom entry | Copper alloy | Painted steel case / safety glass | Vacuum generators, suction circuits, and pneumatic pick-and-place systems |
| 7 | Compound pressure/vacuum gauge | −1–0–3 bar (−14.5–0–43.5 psi) | 2.5 | 100 mm | 1/4 NPT bottom entry | Copper alloy | Painted steel case / safety glass | Circuits that alternate between vacuum and positive gauge pressure |
| 8 | Differential-pressure diaphragm gauge | 0–10 kPa (0–1.45 psi) differential | 2.5 | 100 mm | Two pressure ports; low-range design | Diaphragm and port materials selected for the specified air service | Metal case / clear window | Filter monitoring, ventilation systems, and low-pressure air differential checks |
| 9 | Panel-mount Bourdon tube gauge | 0–6 bar (0–87 psi) | 1.6 | 63 mm | G 1/4 rear entry | Copper alloy | Panel-mount case with bezel / safety glass | Machine control panels and pneumatic skids |
| 10 | Liquid-filled Bourdon tube gauge | 0–10 bar (0–145 psi) | 1.6 | 100 mm | G 1/2 bottom entry | Stainless steel | Stainless-steel case / safety glass; glycerin fill | Installations subject to vibration or pulsation; confirm fill-fluid compatibility and temperature limits |
| Comparison note: These are representative, commonly available specification combinations, not ranked or tied to specific products. Confirm pressure range, connection thread, accuracy, materials, temperature limits, and applicable standards with the supplier for the intended service. Use only gauges compatible with the measured medium and installation conditions. | ||||||||
Industrial pneumatic pressure gauges use several sensing designs, each suited to different operating conditions. Bourdon-tube gauges are common for general compressed-air service. Internal tube movement turns a pointer as pressure changes. Diaphragm gauges use a flexible membrane and can suit lower pressures or systems where a broader sensing surface is useful. Capsule designs also measure low pressures, including some air-handling applications. Small details matter.
The display may be analog or digital. Analog dials are easy to read at a glance, even from a short distance. Digital models can show finer increments, but their batteries and electronics need consideration in maintenance plans. Case and mounting choices matter, too. A panel-mounted gauge keeps readings visible at a machine station, while a rear connection may fit a compact control cabinet. For vibrating lines, a liquid-filled case can steady pointer movement. It is not a cure for every pulsation.
Range selection deserves careful attention. A gauge that runs near its scale limit may be harder to read and more exposed to wear; one with an unnecessarily broad range can hide small changes. Many technicians look for normal operating pressure around the middle portion of the scale, then check the system’s peak pressure and connection requirements. The choice is rarely perfect on paper. Pressure spikes, vibration, temperature, and viewing angle can change what works once the gauge is installed. Calibration records and periodic comparison against a suitable reference help keep readings trustworthy.
Industrial buyers comparing the top 10 pneumatic pressure gauges should start with the measurement task, not the dial style. Dry and liquid-filled gauges suit different vibration conditions; digital models can make readings easier to record. Differential gauges help monitor pressure drops across filters, while panel-mount and back-connected designs fit specific installation layouts. Match the range to normal operating pressure, leaving room for brief surges. A gauge that spends most of its life near the bottom of its scale may be hard to read accurately. Small detail. But it matters.
The U.S. Department of Energy’s Improving Compressed Air System Performance guide notes that leaks can waste 20–30% of compressor output. That figure describes system losses, not gauge error, but reliable pressure readings help teams spot changing conditions and investigate problems. For each candidate, check accuracy class, connection size, wetted materials, case protection, and whether calibration can be verified. Consider dust, pulsation, and the operator’s viewing angle at the actual mounting point. A liquid-filled case may dampen needle movement, yet it can obscure a reading if the gauge is mounted poorly. I would also question whether every measurement point needs a premium instrument. The right choice depends on the process, and that is easy to underestimate.
Top 10 Pneumatic Pressure Gauges for Industrial Buyers
How to Select and Maintain a Gauge for Your Application
Choose a pressure range that keeps normal readings near the middle of the dial, not at its limit. This leaves room for pressure changes and helps prevent repeated over-range readings. Check the gauge’s accuracy against the process requirements, then confirm that its connection size and mounting position suit the equipment. Wetted materials must also tolerate the air, moisture, oils, or cleaning agents present in your system. Readability matters. A large dial can be easier to check from a walkway, while vibration or pressure pulses may call for a protective design or suitable accessories. Small details count.
Before installation or removal, isolate and fully depressurize the line. A gauge should not be treated as proof that a system is safe to open. During routine checks, look for a damaged lens, a bent pointer, corrosion, loose fittings, or a reading that fails to return to zero. Compare important readings with a suitable reference instrument, and record the date and result. Set calibration intervals according to operating conditions, equipment criticality, and the gauge maker’s guidance; one fixed schedule will not suit every plant. In practice, busy teams sometimes postpone checks. That is worth questioning, especially when readings control maintenance decisions. After a repair or suspected overload, recheck the gauge before relying on it.
In a common Bourdon-tube design, compressed air flexes a curved metal tube. A linkage moves the pointer across the dial. It measures pressure at its connection point, not airflow.
Choose a range that keeps normal pressure comfortably within the scale. A needle near the dial’s bottom can make small changes hard to read. Too broad a range may hide them.
It means accuracy of ±0.5% of the gauge’s span. On a 0–10 bar scale, that is about 0.05 bar. Check whether specifications refer to span or reading.
Bourdon-tube gauges suit general compressed-air service. Diaphragm and capsule designs can suit lower pressures. The right choice depends on the system and its operating conditions.
Analog dials are easy to scan from nearby. Digital models can show finer increments, but batteries and electronics require maintenance. The best display depends on where operators read it.
Match the thread type, port position, and wetted materials to the installation. A mismatch can cause leaks or corrosion. Check temperature limits and overpressure ratings, too.
No. It cannot identify a leak by itself. Compare readings at consistent points and operating conditions; pressure changes may signal a need for further investigation.
Vibration can make a pointer harder to read. A liquid-filled case may steady its movement, but it will not fix every pressure pulsation. Field testing matters.
A dial can look convincing while its readings drift out of tolerance. Keep calibration records and compare the gauge periodically with a suitable reference. Even good records need follow-up.
This article explains how a Pneumatic Pressure Gauge measures the pressure of compressed air in industrial systems and why accurate readings matter for safe, reliable operation. It outlines key specifications buyers can compare, including pressure range, accuracy, dial size, connection type, materials, and suitability for different operating conditions. It also introduces common gauge types and designs, showing how their features support different installation and monitoring needs.
A practical overview of ten Pneumatic Pressure Gauge options helps industrial buyers compare features and identify models that fit their applications. The article concludes with guidance on selecting a gauge based on system requirements, installation conditions, and expected performance, along with basic maintenance practices. Regular inspection, careful handling, and timely replacement can help preserve measurement accuracy and extend service life.
Accuracy Instrument